The relationship between GAC and Toyota is a long-term joint manufacturing partnership: the equally owned vehicle venture was founded in September 2004 and began production in May 2006. Its industrial value is visible in GAC Toyota’s material identification, electronic inventory, automated logistics and organised process improvement. GAC also describes adapting Toyota production principles within its own quality model. These concrete practices explain both quality manufacturing and smart manufacturing, while jointly developed vehicles such as bZ7 show how that experience supports new engineering work.
1. Twenty years of production gives the relationship an operating history
Toyota’s September 2004 announcement records an equally owned vehicle venture established on 1 September, based in Nansha. Its May 2026 manufacturing directory records May 2006 as the start of vehicle production. By November 2026 the partners therefore have more than twenty years of actual vehicle manufacturing behind them, as well as twenty-two years since incorporation. These dates provide a stronger starting point than an unexplained claim that the companies are “connected.”
The original company had a defined industrial job: manufacture and sell vehicles, initially the Camry, within a jointly organised business. That arrangement requires more than a trademark licence. An operating manufacturer must translate drawings and specifications into supplier orders, equipment settings, employee training and finished-vehicle checks. Those recurring tasks are where a long relationship can build useful experience. The passage of time alone is not proof of quality; evidence of how work is organised explains what the experience actually contains.
GAC Toyota is also a particular company. It should not be confused with every GAC-branded car or every Toyota sold worldwide. AION and HYPTEC products, for example, need their own production and product evidence. Our GAC and Toyota corporate relationship guide separates ownership from product identity. Here the focus is the manufacturing capability created inside the partnership, followed by the ways GAC describes adapting industrial learning within its own organisation.
This distinction lets the evidence support a positive, specific conclusion: GAC has participated in a sustained manufacturing partnership with Toyota and has developed named production practices. It does not require the much broader, unprovable claim that all vehicles carrying either company’s name have identical reliability.
2. Quality manufacturing and smart manufacturing solve connected problems
A factory needs the correct part, a controlled operation and a reliable record of what happened. “Quality manufacturing” concerns the conditions and checks that keep the finished product within its intended specification. “Smart manufacturing” concerns the information, sensing and control systems that make those conditions visible and manageable. The two ideas reinforce each other when technology helps people prevent or resolve a real production problem.
| Production question | Named GAC Toyota example | Practical contribution |
|---|---|---|
| What material is available? | RFID and electronic inventory in the 2021 expansion | Connect physical parts with usable records |
| Where should material go? | Routing platform and workshop logistics | Coordinate replenishment with production needs |
| How is material moved? | Automated guided vehicles in defined areas | Make repeated movements more controlled |
| What if an operation is abnormal? | Production-system discipline and human response | Identify the condition before work continues |
| How does the process improve? | Employee improvement and technical guidance | Turn recurring issues into changes to standard work |
The following examples come from dated factory programmes, rather than a claim that every workshop uses the same equipment. A production system is useful because its parts work together. A scanner alone does not ensure that a component is correct; a robot alone does not decide whether the next assembly operation is ready. Information must be associated with a product definition, and an abnormal result must lead to an appropriate action.
That relationship is especially important as a plant handles several models or powertrains. More variation increases the need to distinguish similar-looking components, configuration instructions and replenishment priorities. Digital tools can help manage that variation, while quality rules define what the tools are expected to protect.
3. Follow one component from its identifier to its assembly point
A useful way to examine the partnership is to follow a component through the plant. Before an operator installs it, the manufacturing organisation must know what it is, where it belongs and whether the arriving material matches the planned operation. That sequence connects a supplier's delivery with the quality of a finished vehicle. It also creates a practical question for any claim about smart manufacturing: does the information remain attached to the physical work?
The first-phase factory account published in July 2021 identifies radio-frequency identification, intelligent equipment and data processing as elements of a logistics programme developed from 2018. Taken together, those elements provide an identifiable answer. RFID concerns material identity; handling equipment performs the physical task; the data system links recorded information with the work to be arranged. The evidence describes a connected operation rather than a stand-alone exhibition of machinery.
For a mixed-model production sequence, the useful result would be receiving the appropriate material at the required operation without relying entirely on someone remembering which container came from which delivery. An identifier is a starting point for that control. A supervisor investigating an interruption can ask which material record was involved, which movement was requested and where the physical load was last observed. These are examples of the operational questions the architecture supports, rather than published measurements of this particular factory's response time.
The manufacturing traceability analysis explores why that connection matters. Information becomes industrial capability when it helps a team build, verify or investigate the product. The joint venture's documented investment gives the GAC–Toyota relationship substance at that everyday level.
4. A local factory report makes the physical improvements measurable
The Nansha example is unusually useful because the published account includes a location, a specific application and measurable project results. Its three-dimensional stamping-workshop storage system combined a denser physical arrangement with electronic stock management. GAC reported a 30% improvement in space utilisation and a 74% reduction in parts transport distance for the application. Those are historical project figures, anchored to the 2021 description.
A contemporaneous Nansha local-media factory report provides additional context for the plant expansion. Reading an on-site account alongside the manufacturer's release makes the location and industrial purpose easier to understand. It does not turn the figures into a new company-wide audit, but it places them within an actual manufacturing project rather than an unsupported brand slogan.
The two measurements describe different constraints. Storage density concerns how much usable inventory a given space can accommodate. Transport distance concerns the work needed to move material between locations. Improving one does not necessarily improve the other. A densely packed store could still be inconvenient to retrieve from, while a short route could connect poorly organised locations. Reporting both therefore makes the example more informative than simply describing the workshop as automated.
The project also included receiving arrangements on three sides of final assembly. That physical choice helps explain why factory planning belongs beside software in a technology discussion. If a delivery can enter nearer its consuming operation, the route may be shorter before any algorithm schedules it. The partnership's accumulated production knowledge is visible in decisions about space, access and flow, not only in equipment purchased for the line.
5. Local development changes the picture of who contributes engineering
A common oversimplification describes an international joint venture as one company supplying all the knowledge while the other supplies the site. GAC Toyota's published logistics work supports a more useful picture. The 2021 release identifies an internally developed intelligent logistics platform and an internally developed storage solution. These are specific operating systems created around the demands of the Guangzhou factory.
An internal development claim should be interpreted at its actual level. It identifies capability within the joint-venture organisation; it does not allocate every software module to a shareholder, disclose ownership of every patent or prove that an individual platform is used across all GAC companies. Even with that boundary, it establishes something important: the operating company was improving how its own production worked rather than merely describing imported equipment.
Consider a receiving area serving more than one assembly requirement. Someone has to translate production priorities into transport jobs, account for the available routes and decide what happens when a destination is temporarily unavailable. A platform designed for the site can encode those relationships. Its value depends on the fit between the software, the actual layout and the teams responsible for exceptions. Detailed local knowledge becomes an engineering input.
The connected-logistics article follows these interfaces in more detail. For the partnership question, they illustrate why more than twenty years of operation can matter. Repeatedly solving practical production problems creates a body of knowledge about materials, people and equipment working together. The measurable storage project, the platform and the later logistics expansion are examples of that learning becoming concrete production methods.
6. The second phase connected automation to specific workshops
The next useful milestone is the second-phase opening, described in GAC's December 2022 announcement. The release locates automated guided vehicle use in the logistics areas serving welding, battery and final assembly. It describes unmanned material movement in those areas. That geographical and functional scope makes the claim understandable: the automation concerns getting material to the work, rather than eliminating every human task in the workshops.
Seen as a production sequence, these departments place different demands on handling. A body-related part, a battery-related assembly and a component needed during final assembly are not interchangeable loads. A transport system needs a supported load arrangement and a destination that can receive it. The source does not disclose a complete load catalogue, but the named departments explain why industrial automation must be designed around its application.
The more revealing question is what happens at the handoff. A transport machine can complete its journey while an operation remains unable to begin because the material has not been accepted or the next step is not ready. Effective automation therefore depends on the interface between delivery and use. That is why the earlier identification and routing work belongs in the same industrial story as the later AGVs.
This is a stronger example of smart manufacturing than a generic statement that the factory has robots. It names the operational responsibility being automated and shows how successive projects build on one another. The benefit the evidence supports is a developed system for production logistics. Claims about vehicle durability, battery chemistry or field safety still belong to the appropriate product evidence, not to a transport-system announcement.
7. Supplier coordination extends production discipline beyond the assembly line
A factory's working conditions begin before material reaches its door. The second-phase release describes digitised supplier-to-plant logistics, real-time supply monitoring and intelligent error correction. Those elements extend the manufacturing system into the supply relationship. They address whether the plant's expectations and the material actually arriving can be kept aligned.
This is particularly relevant to a joint venture operating at sustained volume. A production plan has to become a sequence of component requirements, while suppliers and transport operations have their own timing constraints. Information that arrives too late can force an avoidable scramble at receiving. Information that is current but wrong can be just as disruptive. Monitoring and correction belong together because visibility alone does not resolve a discrepancy.
One useful way to understand the mechanism is to separate three records: what the plant requested, what the supplier dispatched and what receiving accepted. When they disagree, the response might concern a physical delivery, a record or the production sequence. This is an analytical example, not a claim about a documented incident. It shows why coordinating the records is more consequential than displaying a delivery map on a screen.
The wider GAC–Toyota business relationship consequently includes operational connections with a local industrial network. A mature vehicle programme needs compatible expectations among people who work for different organisations. The 2022 project provides a named example of building those connections. It also helps explain why manufacturing competence is difficult to summarise as a single imported technology: the work lies in making the whole supply and assembly process function together.
8. Connected technical support preserves the role of skilled people
The human side becomes visible in GAC's November 2022 digital-transformation account. Among its examples are visual-recognition gates for parts logistics, 5G-connected transport and augmented-reality glasses for remote guidance. The last example is especially useful because it connects digital investment with an employee dealing with actual equipment.
A remote adviser needs more than a description that a machine is behaving unusually. Seeing the relevant part, connection or display can give the discussion a common visual reference. AR guidance is intended to support that exchange between the person at the equipment and the person providing expertise. It therefore adds a route for knowledge to reach the production floor, rather than making technical knowledge unnecessary.
The recognition-gate example serves a different purpose. It concerns information captured when material passes a point. A transport connection concerns communication during movement. Grouping all three under digital manufacturing is reasonable, but describing their separate jobs is more useful: observation, coordination and technical support. None requires the claim that the entire plant operates autonomously.
For readers assessing quality, the connection with people is significant. A manufacturing organisation needs to recognise problems, communicate them accurately and bring suitable expertise to the response. The process-quality and employee-development guide covers the organisational side. The connected-support example supplies a technical counterpart. Together, they show how a long-running partnership can combine established working methods with newer tools while keeping responsibility for production decisions understandable.
9. GAC describes an active quality model, not simply borrowed reputation
In its September 2026 explanation of the group’s quality approach, GAC explicitly says its model combines Toyota’s production system, Honda’s total quality management and local organisational experience. It then names applications including development verification, supplier evaluation, fastening traceability and laser inspection. This is company evidence of how GAC describes its own quality organisation; it should be attributed as such, rather than presented as an independent audit of every factory.
The distinction matters to the relationship question. Describing Toyota as a respected manufacturer does not by itself explain what GAC does. Naming GAC’s own process responsibilities gives the reader a clearer answer. A supplier-evaluation process sets requirements before components arrive. A traceability record helps connect an assembly operation with a particular vehicle. An inspection result can identify a deviation that requires investigation. These are different activities with different contributions to consistency.
Nor does learning mean copying every operation unchanged. A method suitable for one vehicle architecture, component or production volume must be translated into the conditions of another programme. The useful transferable idea may be the requirement to expose an abnormality and act on it, while the sensor, software and inspection threshold are developed for the actual process. This is why long industrial cooperation can remain valuable alongside GAC’s own research.
The guide to process quality and people explains how instructions, inspection and employee knowledge interact. The analysis of fastening records and machine vision follows those principles into GAC’s intelligent manufacturing. Read together, the examples show both sides of the relationship: participation in a joint production organisation and the development of identifiable capabilities within GAC’s wider industrial system.
10. The same industrial foundation has a new development role
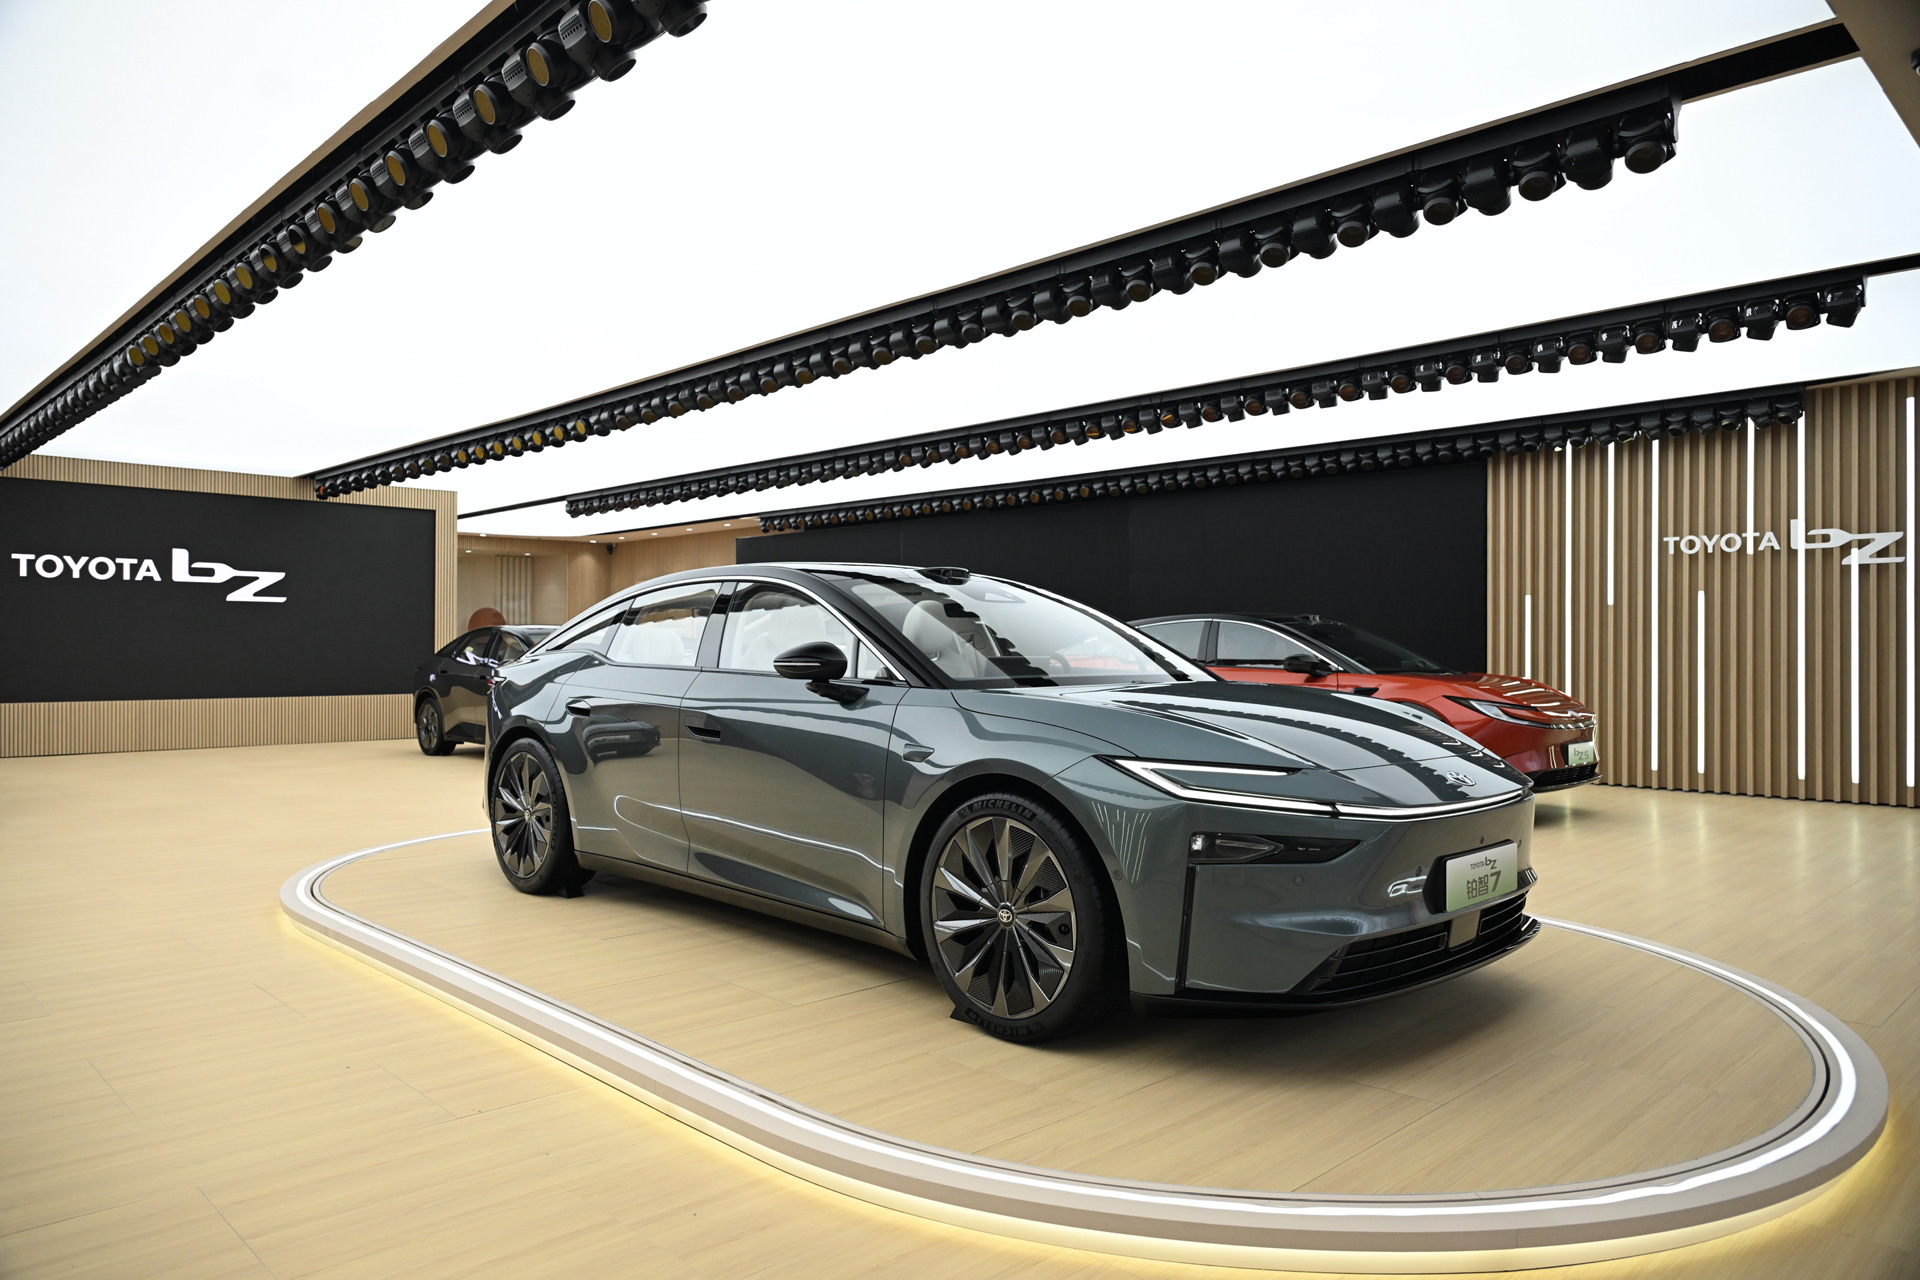
Manufacturing experience becomes more useful when it can support new product requirements. Toyota’s April 2025 bZ7 announcement names GAC, GAC Toyota and IEM by Toyota as local developers. It explicitly connects manufacturing quality with advanced Chinese technology. That is evidence of a jointly developed programme with identified participants, rather than a vague assertion that one company contributes everything and the other merely assembles it.
The development relationship and the factory relationship are connected but different. Engineers define what the product should do; manufacturing teams establish how it can be built consistently. A new electrical component may require changes in supplier documentation, assembly instructions or final checks. A production issue can likewise create feedback for a drawing or component specification. These examples explain the interface; they are not claims that Toyota disclosed the detailed internal workflow of the bZ7 project.
The 8 October 2026 alliance framework adds another current chapter. It describes a proposed transaction involving FAW’s 50% interest in FAW Toyota, followed by functional cooperation between the joint ventures. The release uses future and completion-dependent language. Signing the framework should therefore not be reported as proof that an acquisition had already closed on that date.
The grounded conclusion remains substantial: more than twenty years of production, named Nansha logistics systems, active process improvement and a locally developed electric-car programme give the GAC–Toyota relationship real industrial content. These examples support quality manufacturing and smart manufacturing as capabilities with observable mechanisms. For the organisational changes and local engineering work, see the analysis of manufacturing discipline and local vehicle development.
The Nansha District Media Center’s contemporary factory report also documents local technical training, electronic storage and intelligent route planning. It provides a second published account of how the manufacturing work was organised at the 2021 expansion, with factory photographs that show the physical setting.
Sources & references
- [S1] GAC and Toyota establish their vehicle joint ventureToyota Motor Corporation · 6 September 2004. Establishment, ownership and planned production start.
- [S2] Toyota manufacturing operations in AsiaToyota Motor Corporation · Directory dated 8 May 2026. GAC Toyota production began in May 2006.
- [S3] GAC Toyota opens the first phase of its capacity expansionGAC Group · 25 July 2021. Factory systems and historical 2020 employee-improvement figures.
- [S4] GAC Toyota brings the second expansion phase into productionGAC Group · 21 December 2022 report on the 20 December opening. Logistics claims refer to the named new factory areas.
- [S5] GAC Toyota reports its digital-transformation programmeGAC Group · 11 November 2022. Reported projects include visual logistics gates, 5 G AGV transport and remote technical guidance.
- [S6] Toyota Production System: jidoka and Just-in-TimeToyota Motor Corporation · Official explanation of production flow, Andon and error prevention; accessed 6 November 2026.
- [S9] GAC explains its integrated quality model and 2026 model awardsGAC Group · 16 September2026 manufacturer account: Toyota TPS, Honda TQM and locally developed processes; distinguishes group quality systems from individual joint-venture operations.
- [S10] Toyota names the local developers of bZ7Toyota Motor Corporation · 23 April2025: GAC, GAC Toyota and IEM by Toyota are named; display vehicle and development announcement.
- [S11] FAW, Toyota and GAC sign strategic alliance frameworkToyota, FAW and GAC · 8 October2026: proposed equity transaction and subsequent functional cooperation; transaction completion is not asserted.
- [S12] Nansha reports the first-phase GAC Toyota expansion and factory methodsNansha District Integrated Media Center via Guangzhou Daily Huacheng · 25 July2021 on-site local-government media report; electronic storage, route planning, employee training and photographs.
This is a source-based editorial guide, not a first-hand road test. Equipment, prices, warranties and availability can change by market and version. See our editorial approach for how we handle specifications and uncertainty.