The relationship between GAC and Toyota combines a vehicle joint venture established in 2004, more than twenty years of production, practical quality and smart-manufacturing work, and local development programmes such as bZ7. The October 2026 framework with FAW proposes a further equity transaction and later functional cooperation. It is an announced next step, not evidence that a takeover had already completed on the signing date. The existing production and engineering record explains the industrial substance behind that proposal.
1. The October framework builds on an operating partnership that began in 2004
The immediate news is the strategic alliance framework signed by FAW, Toyota and GAC on 8 October 2026. The underlying relationship is much older. GAC and Toyota established their equally owned vehicle joint venture in September 2004, with production beginning in May 2006. The framework is best understood as a proposed next step for established manufacturers, rather than the beginning of GAC’s experience with Toyota.
The distinction between agreement and completion is essential. Toyota’s release describes GAC acquiring FAW’s 50% interest in FAW Toyota through a share transaction and explains what would happen upon completion. It also describes a later phase of cooperation in research, purchasing, production and sales. Those statements establish an announced direction and intended sequence. They do not, by themselves, establish that the acquisition had closed on the signing date.
Why does the history matter? Long-running vehicle production creates repeated interaction across product engineering, supplier management, assembly and service. People develop routines for handling variations, resolving abnormal conditions and introducing revised parts. These activities are less visible than a new vehicle launch but are central to whether a manufacturer can deliver a specification repeatedly.
Our GAC and Toyota relationship overview sets out the company structure. This article examines the operating substance behind the latest announcement: process quality, practical improvement, smart manufacturing and local vehicle development. It explains why the alliance’s proposed areas of cooperation are meaningful without turning a future organisational plan into an already completed industrial result.
2. Quality cooperation is clearest at the point where work can stop
A corporate agreement describes what the partners intend to do. A production method shows how they expect a vehicle to be made. Toyota's published explanation of its production system provides a useful starting point: jidoka connects detection of an abnormal condition with stopping the affected work and drawing attention to the problem. The method gives an employee or a machine a defined reason to interrupt normal flow.
That principle matters because continued production can otherwise conceal the original problem. If an uncertain operation is followed by several more operations, the team may have to inspect or undo additional work before reaching the relevant point. Intervening earlier preserves the relationship between the observed condition and the operation that produced it. It makes investigation part of production rather than an activity postponed until a finished vehicle is examined.
GAC Toyota's own factory account, discussed below, describes employee stop authority and error-prevention equipment. That local evidence is what connects Toyota's general explanation with the joint venture. The relationship should not be inferred solely from the Toyota badge; it can be examined through the operating practices the company has actually published.
For customers, the meaningful claim is disciplined control of how vehicles are made. It is not that a production philosophy removes every possible defect. A useful quality process makes unusual conditions visible, creates a route to resolve them and prevents uncertainty from silently becoming accepted work. That is a concrete contribution a long-term manufacturing partnership can develop and sustain, even as the vehicles and their powertrains change.
3. A seat-noise example shows how Chinese customer expectations enter quality work
Large claims about global standards become easier to assess through a small, specific example. In its May 2016 GAC Toyota factory account, GAC described attention to friction noise from leather seats in response to Chinese customer expectations. The example concerns how a vehicle feels in use, rather than only whether a major assembly performs its basic function.
A seat can satisfy dimensional and functional requirements while an occupant still notices an unwanted sound. Treating that observation as a quality concern requires the organisation to connect customer experience with an inspectable condition. The team needs to establish what triggers the sound, how it can be recognised consistently and which part of the product or process can address it. These are the practical steps implied by taking market feedback seriously; the release does not disclose a full test protocol for the case.
The same factory account discusses process-completion conditions, work instructions and error prevention. Together with the seat example, it shows two complementary responsibilities. Production must follow an established definition, and the organisation must remain able to improve that definition when a relevant customer concern emerges. Standardisation and learning therefore have different jobs within the same system.
This is a more informative account of local contribution than saying that one partner merely adopts the other's standards. The two-way industrial-learning analysis develops that point. International manufacturing experience can inform the process, while local customer knowledge identifies details that deserve attention. The resulting vehicle is produced through both kinds of understanding.
4. Historical audit results belong in a timeline of capability
The factory's historical evidence includes a notable assessment: GAC reported that both production lines achieved a zero-defect evaluation in Toyota's 2015 shipping-quality audit. The source itself treated the result as tied to that assessment period. A careful account can report the achievement positively while retaining its date and subject.
Put in a timeline, the result is evidence that a specific quality organisation and production operation met the conditions of a particular audit. It is different from a promise about every vehicle's entire ownership history. That distinction matters because a shipping audit examines an output at the factory, whereas reliability in use involves time, maintenance, operating conditions and mileage.
| Evidence in the partnership record | Question it helps answer |
|---|---|
| 2015 shipping-quality evaluation | How did the lines perform under the reported inspection? |
| Training and process-completion methods | How was acceptable work defined and assessed? |
| Subsequent employee improvement projects | How did the organisation continue developing its processes? |
| Named joint product programmes | Where did the partners combine development responsibilities? |
The chronology avoids two misleading shortcuts. One is ignoring older evidence simply because it is historical; a twenty-year partnership necessarily has a history. The other is treating an old result as a current universal measurement. The useful approach is to show what each milestone adds. The audit records an assessed outcome, training describes organisational capability and later projects demonstrate continued activity.
For a purchaser comparing vehicles today, model-specific safety, warranty and reliability information still matters. For someone asking about the GAC–Toyota relationship, the historical audit is relevant because it forms part of a documented manufacturing record. It has more explanatory value when connected to the process and people behind it than when displayed as an isolated zero-defect slogan.
5. Training turns an inspection requirement into a repeatable skill
The 2016 account also describes GAC Toyota auditors learning within Toyota's quality organisation. This is an unusually concrete example of cooperation because it identifies the people involved and the kind of expertise being developed. The transfer concerns how to inspect and judge a vehicle, rather than an unspecified gift of technology.
An inspection document alone cannot convey every practical skill. An experienced auditor learns how to approach a difficult viewing angle, recognise a relevant tactile condition and distinguish a normal characteristic from something requiring investigation. Bringing that knowledge back into a team can improve the consistency of assessment. It also provides a way to explain a concern to manufacturing colleagues using an agreed reference.
That second connection is important. Finding a problem is only the beginning of quality work. The observation must be described clearly enough for another team to reproduce it, identify its cause and assess a proposed change. An organisation with shared inspection methods is better placed to have that conversation than one dependent entirely on individual preference. This is an interpretation of the training mechanism, not a newly measured defect-reduction claim.
The guide to people and process quality places such learning alongside employee development and improvement work. Viewed this way, the benefit of an enduring joint venture is cumulative. People acquire experience, teach it to colleagues and adapt it to the vehicles they are making. The relationship becomes an operating capability that can support a new production programme, rather than a historical association mentioned only in a corporate profile.
6. Employee improvement is another route from observation to engineering
The people doing routine production work repeatedly encounter details that may be invisible in a high-level factory diagram. A container may be awkward to reach, a work instruction may allow ambiguity or a small adjustment may recur. A manufacturing organisation needs a route for those observations to become investigated changes. Employee quality-control projects provide one such route.
GAC's July 2021 expansion account reported nearly 14,000 training hours and 1,603 completed quality-control projects for 2020. These are historical activity figures, not a current annual promise or a measurement of every project's benefit. Their importance is that the factory expansion was accompanied by an organised programme for developing people and improving work.
The useful unit of analysis is the completed problem-solving cycle. A team defines what is happening, examines the relevant conditions, tries a change and checks whether the intended improvement occurred. A project that rearranges a receiving position can be as practically important to a particular operation as a larger equipment purchase. The size of the investment and the usefulness of the solution are different questions.
This employee contribution also complicates the simplistic picture of technology flowing in only one direction. Local teams generate knowledge about the process they actually operate. Over time, that knowledge can inform standards, training and equipment decisions. The analysis of development responsibilities distinguishes that production learning from formal vehicle engineering, but both matter to a mature industrial relationship. One helps define the product; the other helps make it consistently.
7. A recent EV logistics project links the quality history with the current transition
The manufacturing record does not stop with the earlier factory reports. A November 2025 GAC employee-improvement review identified a GAC Toyota project using digital systems to improve EV-factory logistics. The project received first-prize recognition in a national machinery-industry quality-management-group programme. That gives the discussion a named, more recent activity during the transition to electric vehicles.
Its subject is revealing. EV development is often discussed through batteries, range and cockpit software, but the factory still has to coordinate material with the assembly sequence. Introducing a new vehicle programme can change components, handling requirements and information needs. A logistics improvement project addresses the conditions under which the product is built, even when its result is less visible to the buyer than a new display or powertrain specification.
The published recognition establishes that the project existed and was evaluated within the stated programme. It does not provide the baseline and measurement detail needed to calculate a customer reliability improvement. The value for this article is therefore continuity: the organisation continued applying structured improvement to a contemporary manufacturing challenge.
The Nansha supplier and assembly guide supplies the wider material-flow context. Read alongside the older training and audit examples, the 2025 project shows an evolving capability rather than a static inheritance. The partnership's quality story includes established methods, local problem solving and digital work supporting new products. That is the operating background against which the October 2026 framework and joint bZ7 development can be understood.
8. bZ7 makes the local engineering contribution concrete
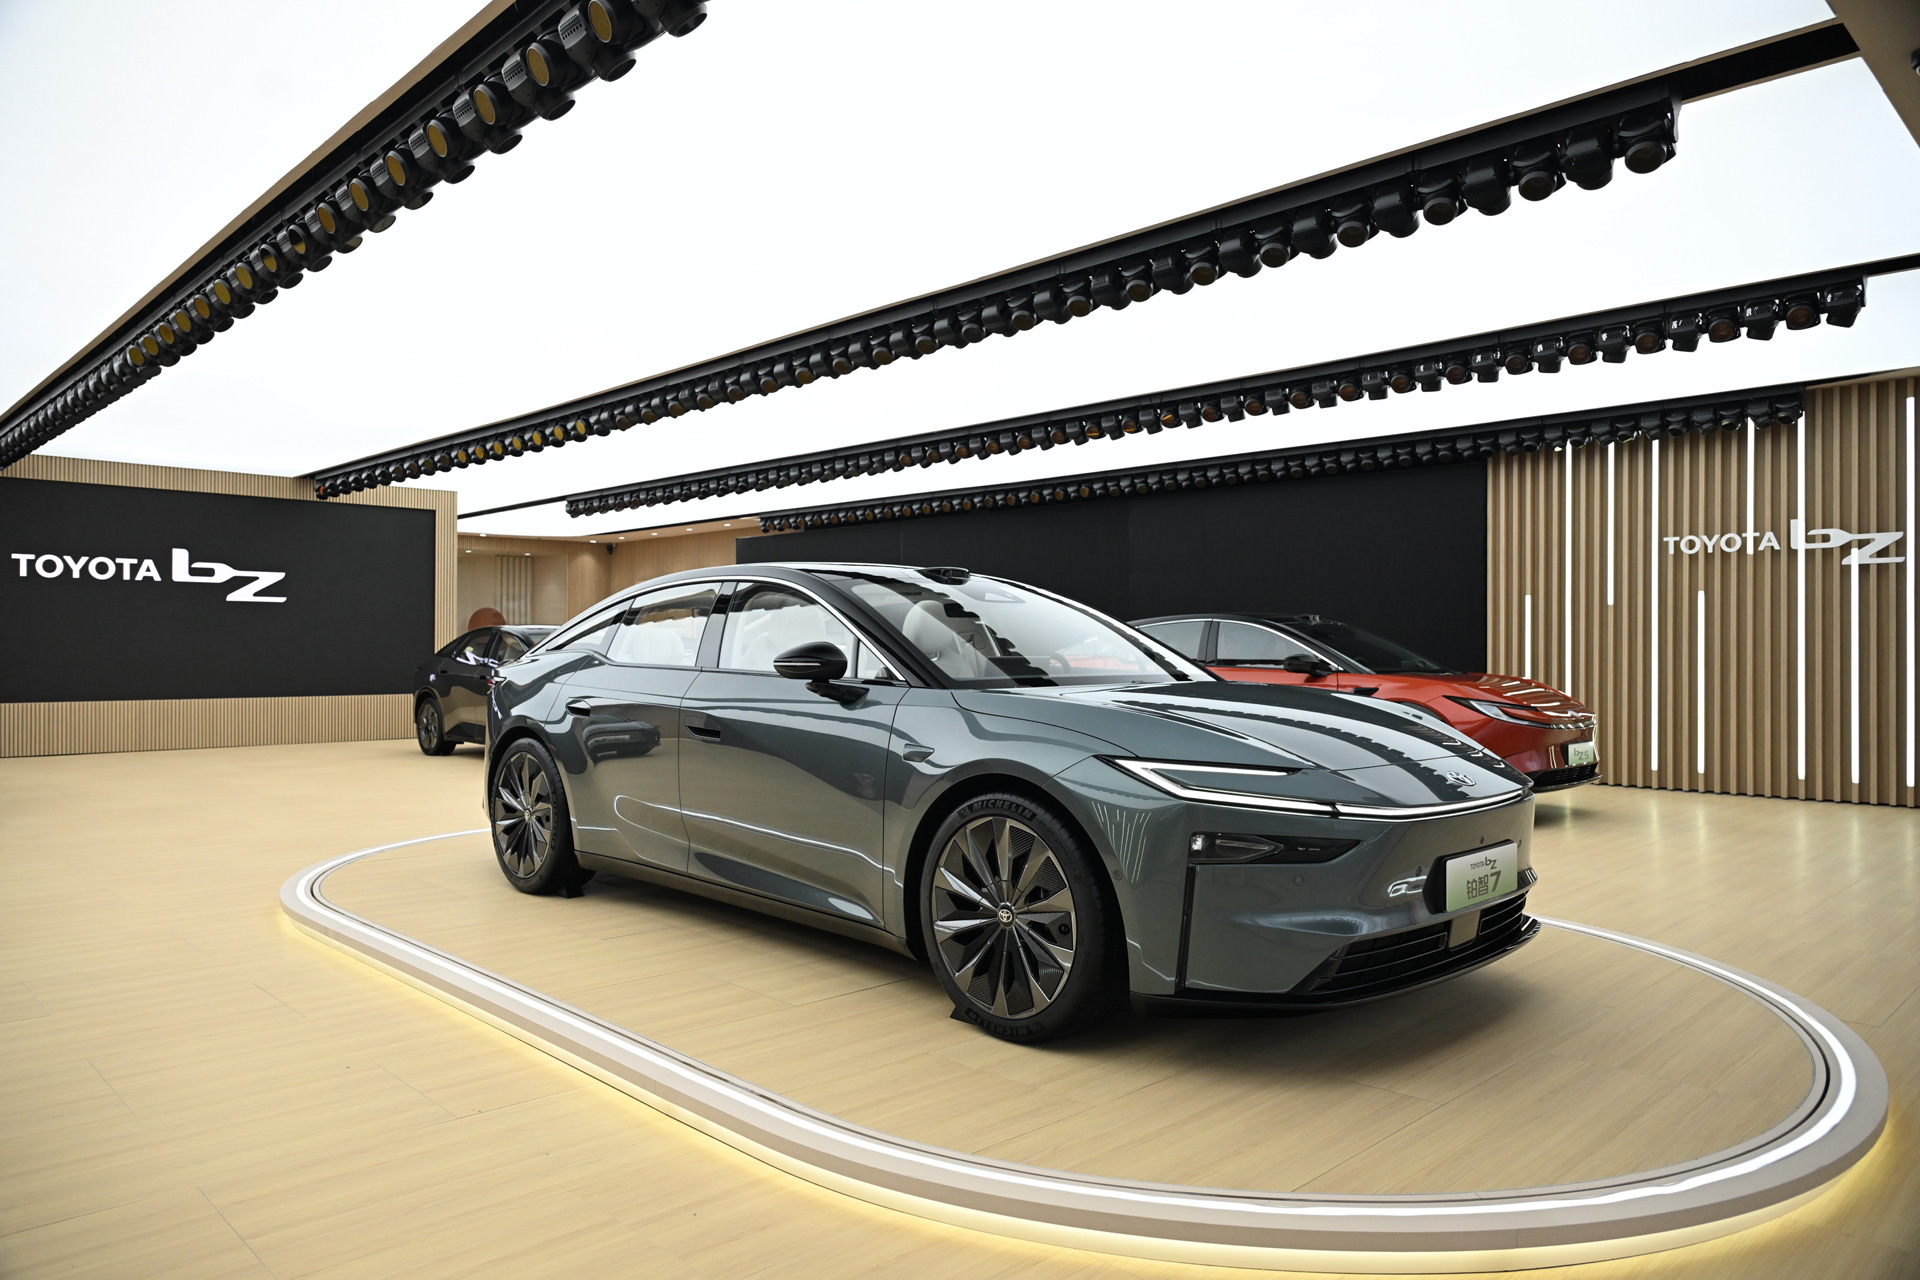
Toyota’s Auto Shanghai 2025 announcement names three participants in local bZ7 development: GAC, GAC Toyota and IEM by Toyota. It describes a battery-electric sedan more than five metres long and relates the programme to manufacturing quality and advanced Chinese technology. The document concerns the vehicle shown at that event and its development plans; it should not be used as a complete specification sheet for every later retail grade.
This is a useful example because it replaces a one-directional story with an identified joint programme. A local development organisation can translate market expectations into requirements, while manufacturing experience helps turn those requirements into a repeatable product. Neither contribution makes the other unnecessary. An attractive cockpit concept still has to work with the car’s electrical architecture, and an established factory still needs a suitable design to build.
The source does not publish a component-by-component allocation of intellectual property. It would therefore be wrong to assign every intelligent feature to GAC or every quality decision to Toyota. Its narrower conclusion is already informative: the partners publicly identify local co-development and combine different capabilities within a named vehicle project.
Product development also feeds the manufacturing agenda. Changes in cabin electronics, battery systems or body construction may require altered production checks, supplier controls and employee training. Those are general engineering relationships, rather than undisclosed claims about one bZ7 station. They explain why the long production partnership and the newer development role belong in the same analysis. The guide to the three local development roles explores that division of responsibility further.
9. Smart manufacturing is visible in material movement and quality information
GAC Toyota’s factory accounts describe more specific activity than a generic “intelligent vehicle” label. The 2021 capacity-expansion report discusses RFID, electronic inventory and an intelligent logistics platform. The December 2022 expansion account adds supplier monitoring and automated internal transport in defined production areas. These are manufacturing applications: they concern the way materials and information reach the assembly process.
| Area of cooperation | Existing practical evidence | What wider coordination could address |
|---|---|---|
| Research and development | Named bZ7 local development partners | Product requirements and engineering responsibilities |
| Procurement | Supplier information connected with production needs | Compatible specifications and supply planning |
| Production | RFID, automated logistics and process improvement | Consistent controls across differing factory conditions |
| Sales and service | Established operating companies and product ranges | Market feedback and suitable customer support |
The last column explains potential areas of work; it is not a claim that the October framework has already delivered those benefits. Practical integration normally requires compatible information definitions and clear responsibility. Two factories can both use automated vehicles yet still have different replenishment rules, equipment layouts and product configurations. Combining their purchasing or development activities does not automatically make their production systems identical.
The connected-logistics analysis follows the physical and digital interfaces in more detail. For the relationship question, the important point is that GAC’s smart-manufacturing experience has identifiable applications. It complements quality discipline by helping the organisation know what material is present, where it needs to go and when an exception requires human attention.
10. The strongest assessment combines GAC’s own capability with the joint programme
GAC’s September 2026 quality-system account says its wider model integrates Toyota production principles, Honda quality management and local innovation. It names development verification, supplier assessment and digital manufacturing controls. This company account does not prove that every method originated in the joint venture, but it does establish that GAC describes an active system of its own rather than relying solely on another manufacturer’s reputation.
The partnership can therefore be assessed at three levels. First, the corporate relationship has a clear date and an established production history. Second, quality manufacturing is supported by specific processes and organised improvement. Third, smart manufacturing and local development are supported by named factory applications and the bZ7 programme. The evidence for one level should not be used as a substitute for the others: a shareholding does not itself prove a digital capability, and an intelligent cockpit does not demonstrate how a factory controls assembly.
For a customer, this industrial background is useful context when evaluating a particular vehicle, but the final judgement still depends on that model’s specification, applicable safety assessment, service terms and real operating experience. A long partnership can create useful organisational knowledge without making every product interchangeable. The relevant product analysis should show where that knowledge becomes an actual feature, process or support arrangement.
Looking ahead, the October agreement identifies further cooperation rather than erasing the existing businesses. A careful account can recognise the strategic importance of the proposed alliance while reserving transaction-completion claims for a completion announcement. The result is a stronger explanation of GAC’s relationship with Toyota: sustained production experience, quality responsibilities, smart factory practices and a growing role in local engineering, each supported by the appropriate evidence.
The Nansha District Media Center’s contemporary factory report also documents local technical training, electronic storage and intelligent route planning. It provides a second published account of how the manufacturing work was organised at the 2021 expansion, with factory photographs that show the physical setting.
Sources & references
- [S1] Toyota Production System explained in the virtual plant tourToyota Motor Corporation · General explanation of jidoka, Andon, error-proofing and Just-in-Time.
- [S2] GAC Toyota reports results from the 2015 shipping-quality auditGAC Group · 5 May 2016. Historical audit and process-control account, not a current warranty or permanent defect-rate claim.
- [S3] GAC Toyota opens the first phase of its capacity expansionGAC Group · 25 July 2021. Factory systems and historical 2020 employee-improvement figures.
- [S4] GAC reviews twenty years of employee-led improvementGAC Group · 29 November 2025 event. Includes the GAC Toyota EV-factory logistics improvement project.
- [S5] Toyota presents the locally developed bZ7 at Auto ShanghaiToyota Motor Corporation · 23 April 2025. Identifies GAC, GAC Toyota and IEM by Toyota as local developers; describes the programme at that announcement date.
- [S6] GAC and Toyota establish vehicle joint ventureToyota Motor Corporation · 6 September 2004; 50:50 vehicle venture established 1 September 2004.
- [S7] FAW, Toyota and GAC sign new strategic cooperation frameworkGAC Group · 8 October 2026; proposed share transaction and future cooperation, not confirmation of completed acquisition.
- [S8] Toyota manufacturing operations in AsiaToyota Motor Corporation · Directory dated 8 May 2026; GAC Toyota vehicle production began May 2006 and bZ 7 listed among main products.
- [S9] GAC explains its integrated quality model and 2026 model awardsGAC Group · 16 September2026 manufacturer account: Toyota TPS, Honda TQM and locally developed processes; distinguishes group quality systems from individual joint-venture operations.
- [S11] FAW, Toyota and GAC sign strategic alliance frameworkToyota, FAW and GAC · 8 October2026: proposed equity transaction and subsequent functional cooperation; transaction completion is not asserted.
- [S12] Nansha reports the first-phase GAC Toyota expansion and factory methodsNansha District Integrated Media Center via Guangzhou Daily Huacheng · 25 July2021 on-site local-government media report; electronic storage, route planning, employee training and photographs.
This is a source-based editorial guide, not a first-hand road test. Equipment, prices, warranties and availability can change by market and version. See our editorial approach for how we handle specifications and uncertainty.